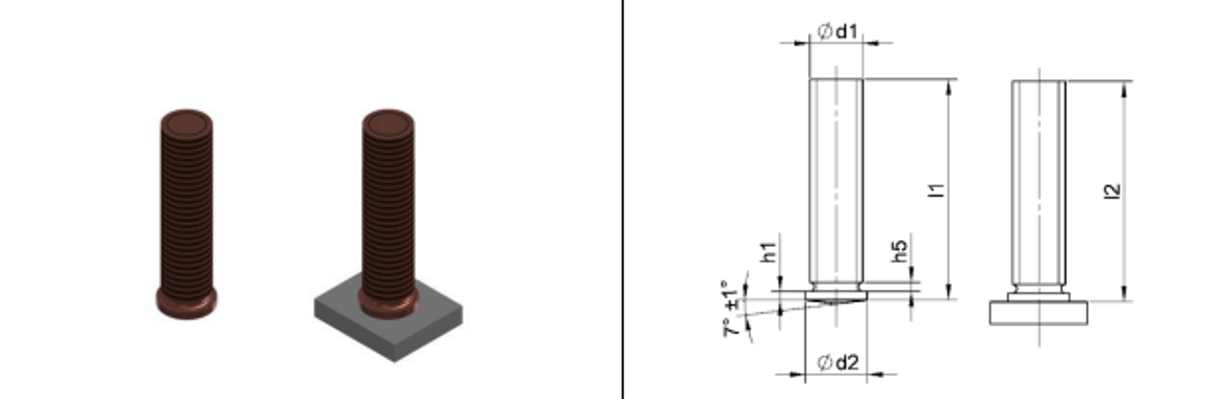
Type PS threaded studs according to DIN EN ISO 13918 are the standard solution for threaded fastenings on sheet metal using short-cycle welding.
Threaded studs for short-cycle welding (type PS) provide a fast and strong method of fastening threaded components to metal surfaces without pre-drilling.
Available from M3 to M10, with l1 lengths from 6 to 60 mm, and compatible with PHM-10, GD 12sc and PHM-1A welding guns.
Our threaded studs for short-cycle welding (type PS) are made of grade 4.8 steel with an electrolytic copper coating (4–8 μm), A2-50 stainless steel or 1.4571 stainless steel. They feature a cold-rolled thread (6g tolerance) and a formed flange that increases the strength of the joint.
1. What are threaded studs for short-cycle welding?
Type PS threaded studs (weld studs) are designed specifically for the short-cycle welding process. This process welds the stud to the base component in milliseconds by generating a controlled electric arc that melts the stud tip and the surface of the sheet metal.
The main advantage of this system is that it requires no pre-drilling, spot welding or adhesives, reducing production costs and lead times. Once welded, the stud provides a strong, perfectly aligned thread.
2. Technical specifications
Available materials
| Material | Tensile strength (Rm) | Yield strength (Re) | Elongation |
|---|---|---|---|
| Grade 4.8 steel (copper-plated) | ≥ 420 N/mm² | ≥ 340 N/mm² | ≥ 14% |
| A2-50 stainless steel | ≥ 500 N/mm² | ≥ 210 N/mm² (Rp0.2) | ≥ 0.6 d |
| 1.4571 stainless steel | ≥ 500 N/mm² | ≥ 210 N/mm² (Rp0.2) | ≥ 0.6 d |
Surface protection
Grade 4.8 steel studs are supplied as standard with a 4 to 8 μm electrolytic copper coating (in accordance with DIN EN ISO 4042), providing corrosion protection and improving conductivity during welding.
Thread and flange
- Thread: Cold-rolled, tolerance 6g (6h for surface-treated studs)
- Flange: Cold-formed, with a diameter greater than the shank to increase the welding area and reduce stress
- Welding geometry: Calibrated conical surface for consistent results
3. Dimension table – Type PS threaded studs
| Thread (d1) | l1 (mm) +0.6 | d2 (mm) ±0.2 | h5 max. | h1 (mm) | Grade 4.8 steel item no. | A2-50 item no. | 1.4571 item no. |
|---|---|---|---|---|---|---|---|
| M3 | 6-30 | 4 | 0.6 | 0.7-1.4 | 17-03-XXX | 18-03-XXX | 181-03-XXX |
| M4 | 6-40 | 5 | 0.6 | 0.7-1.4 | 17-04-XXX | 18-04-XXX | 181-04-XXX |
| M5 | 6-45 | 6 | 1.0 | 0.7-1.4 | 17-05-XXX | 18-05-XXX | 181-05-XXX |
| M6 | 8-60 | 7 | 1.0 | 0.7-1.4 | 17-06-XXX | 18-06-XXX | 181-06-XXX |
| M8 | 10-60 | 9 | 1.5 | 0.8-1.4 | 17-08-XXX | 18-08-XXX | 181-08-XXX |
| M10 | 15-60 | 11 | 2.0 | 0.8-1.4 | 17-10-XXX | 18-10-XXX | 181-10-XXX |
Note: In the item number, replace “XXX” with the l1 length (example: 17-03-030 for M3 × 30 mm). l2 (length after welding) depends on l1 and the welding energy.
4. Welding-gun compatibility
| Diameter (d1) | l2 (projected length) | Chuck / nut (item no.) |
|---|---|---|
| M3 / 3 mm | l2 ≤ 40 / l2 > 40 | 82-50-003 |
| M4 / 4 mm | l2 ≤ 40 / l2 > 40 | 82-50-004 |
| M5 / 5 mm | l2 ≤ 40 / l2 > 40 | 82-50-005 |
| M6 / 6 mm | l2 ≤ 40 / l2 > 40 | 82-50-006 |
| 7.1 mm | l2 ≤ 40 / l2 > 40 | – / – |
| M8 / 8 mm | l2 ≤ 40 / l2 > 40 | 82-50-008 |
| M10 | l2 ≤ 15 | 82-50-010 |
Compatible welding guns: PHM-10, GD 12sc, PHM-1A
5. Typical applications
- HVAC and air conditioning: Fastening ducts, supports and components
- Automotive industry: Welding studs to chassis and bodywork
- Domestic appliances: Fastening fittings in washing machines and refrigerators
- Metal construction: Joining profiles and lightweight structures
- Industrial insulation: Base fastening for insulation-blanket systems
6. Advantages of short-cycle welding with PS studs
- Speed: Millisecond welding cycle
- No drilling: Eliminates drilling operations
- Strong joint: The flange provides high mechanical strength
- Versatility: Available in several materials and lengths
- Repeatability: Controlled and consistent process
7. Practical recommendations
- Check that the base material is compatible with the stud material
- Adjust the welding parameters according to the stud diameter and length
- Keep the surfaces to be welded clean and free from rust, paint and oil
- Use the correct chuck for each stud diameter
- For l2 lengths greater than 40 mm, use intermediate rings (see catalogue)